N52 Ring Magnets — Custom Sintered NdFeB Torus
What N52 can and cannot do in a ring
N52 is the highest-flux sintered grade and also the least heat-tolerant one. Its measured remanence is 1,420 mT, intrinsic coercivity is ≥ 955 kA/m, maximum energy product is ≥ 390 kJ/m³, and its maximum operating temperature is 60 °C — against 80 °C for N35–N48. A buyer who specifies N52 for a ring that will sit near a motor winding or under a heat-generating coil is buying more flux than the assembly can keep. Where temperature is the binding constraint, we move the ring to an H, SH or UH grade and accept slightly lower flux.
Diametral and radial magnetization are not the same
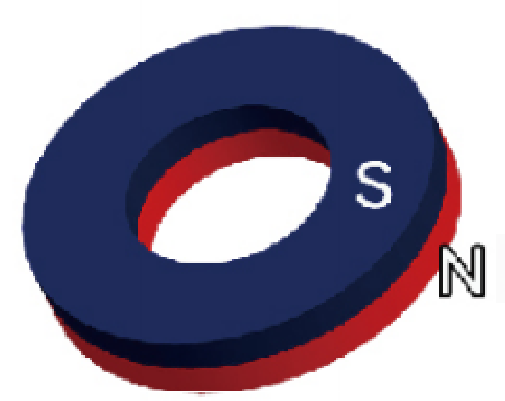
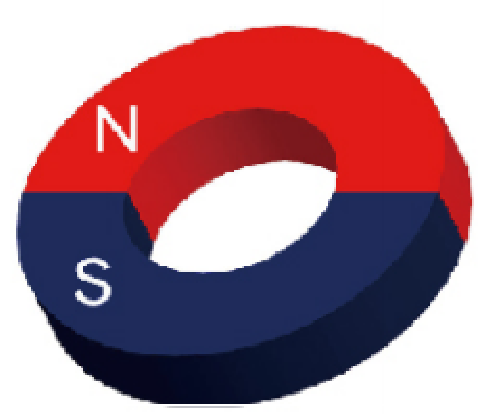
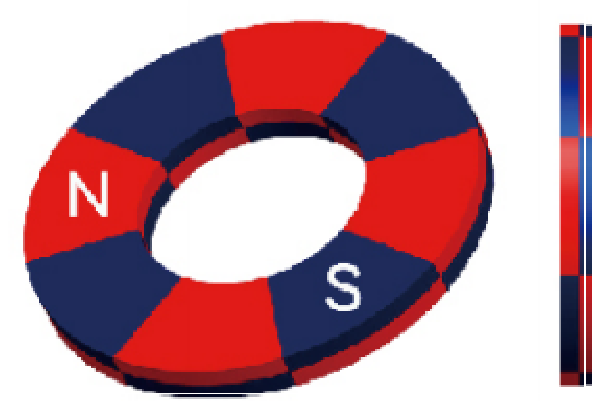
A ring can be magnetized axially (poles on the two flat faces), diametrically (north on one side of the ring, south on the other, across the diameter), or radially and multi-pole around the circumference. The choice changes the field shape and therefore the application: diametral rings suit position sensing and magnetic couplings, while multi-pole radial rings suit small motors and magnetic encoders. We produce radial, axial, diametral and custom multi-pole patterns, plus dedicated magnetization fixtures where a pattern has to repeat precisely.
Dimensions and tolerance
Rings are quoted on OD, ID and thickness — the three dimensions that define the part, and usually the three critical ones. Standard tolerance is ±0.05 mm; critical dimensions can be held to ±0.02 mm. Because the ID is a bored feature, we confirm which of the three dimensions is functional before quoting, rather than applying one tolerance to all of them.
Coating and surface
Ni-Cu-Ni is the default for a general-purpose ring; black nickel, zinc, tin, gold, silver, black epoxy and phosphating are all available and are selected against the environment. Gold and silver are typically specified for contact or cosmetic reasons rather than corrosion alone. Salt-spray duration is quoted per coating across 12–96 hours.
Inspection and lead time
Each batch passes dimensional, flux, coating-thickness, salt-spray and pull-force checks plus a 100 % final inspection. Samples 10–15 days, small batches 20–30 days, mass production 40–60 days; in-stock samples are free, freight only. Send OD / ID / thickness, grade, magnetization direction and coating, and we return a quote and a feasibility answer within one business day.
Available magnetisation directions — Ring magnets
The magnetisation direction is fixed when the magnet is magnetised and cannot be changed afterwards, so the direction must be confirmed before production.


Manufacturing capability & measured data
Tolerance
- Standard production
- ±0.05 mm
- Critical dimensions (on request)
- ±0.02 mm
Quoted per dimension against international dimensional quality standards, not as one blanket percentage. ±0.05 mm is the standard band; where a drawing calls for more, critical dimensions are held to ±0.02 mm using grinding or wire-cutting. The final tolerance is confirmed against your drawing before production.
Salt spray
- Duration depends on coating
- 12 – 96 h
Tell us how many hours your application needs and we match the coating to it. The test standard and the hours each coating reaches are confirmed on request.
Lead time
- Sample
- 10 – 15 days
- Small batch
- 20 – 30 days
- Mass production
- 40 – 60 days
Bands are by order type, not a single quantity threshold; exact lead time is confirmed at quotation.
Measured N52 properties
- Remanence Br
- 1,420 mT
- Intrinsic coercivity Hcj
- ≥ 955 kA/m
- Max energy product BHmax
- ≥ 390 kJ/m³
- Max operating temperature
- 60 °C
N52 has the highest flux of the sintered grades and the lowest heat tolerance: its maximum operating temperature is 60 °C, against 80 °C for N35–N48. For higher temperatures we move to an H, SH or UH grade and accept slightly lower flux.
Catalogue range and specialty grades
- Standard catalogue range
- N35–N52 (M–AH series)
- Specialty grade, on request
- N54 / N55
- Designation
- N54 (China) · N55 (international)
Related Products
- Disc N35 N52 10x2 10x3 12x2 12x3 15x2 16x3 Mm
- Full Customized N35 N38 N42h Arc Tile Strong
- Advanced Technology Magnetic Levitation Float
- Powerful Ndfeb Magnet D25mm N52 Disc Countersunk
- Arc Magnet N35 N52 Strong Motor Materials
- N52 Custom Round Industrial Nickel Coated Ndfeb