Full Customized N35 N38 N42h Arc Tile Strong
An arc segment is a dimensional part
An arc segment is a dimensional part, not a material part. Two suppliers can use the same grade and the same coating, and one motor will still run quieter than the other, because what differs is whether the segment's inner radius actually matches the rotor's outer radius and whether the arc angle repeats. Arc and tile magnets are therefore quoted against your drawing, dimension by dimension — not as one blanket percentage.
Common grade combinations
N35, N38 and N42H are the common starting points for arc segments: N35 where cost dominates, N38 as the general-purpose middle, and N42H where the segment has to hold flux at an elevated housing temperature. Grades from N35 to N52 are available across the M, H, SH, UH, EH and AH series, so an arc can be re-graded without changing the tooling.
Shapes and geometry
Beyond simple arcs we cut trapezoid segments, curved tile geometries, U-shape arcs and other non-standard outlines from your drawing. Because the magnets are pressed and then machined, an unusual outline is a machining question rather than a new process.
Dimensional control
Standard tolerance is ±0.05 mm; critical dimensions on a segment — typically the inner radius and the chord — can be held to ±0.02 mm with grinding or wire-cutting. Segment-to-segment consistency is what controls cogging, so the drawing review starts with which dimensions matter.
Magnetization and coating
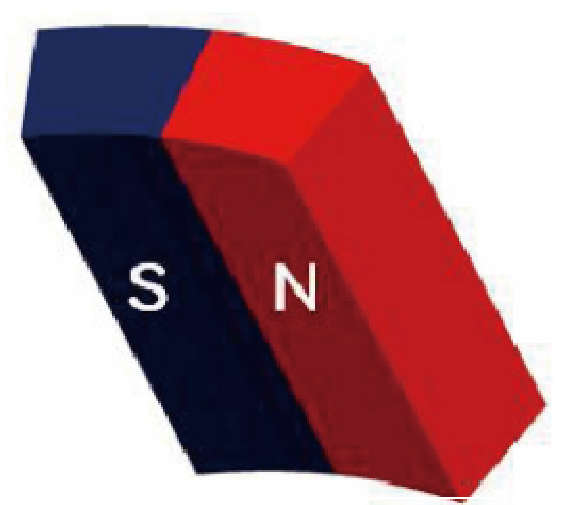
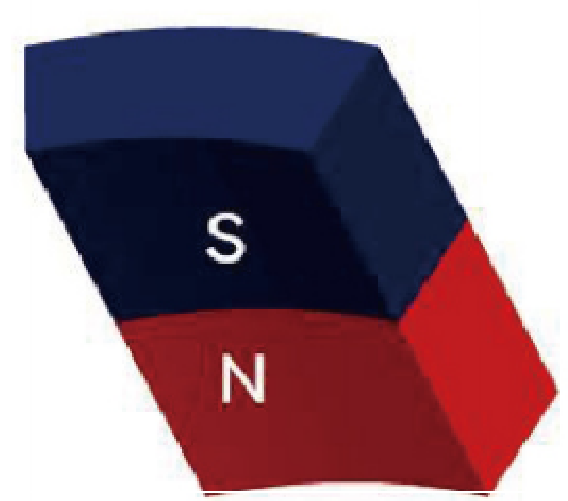
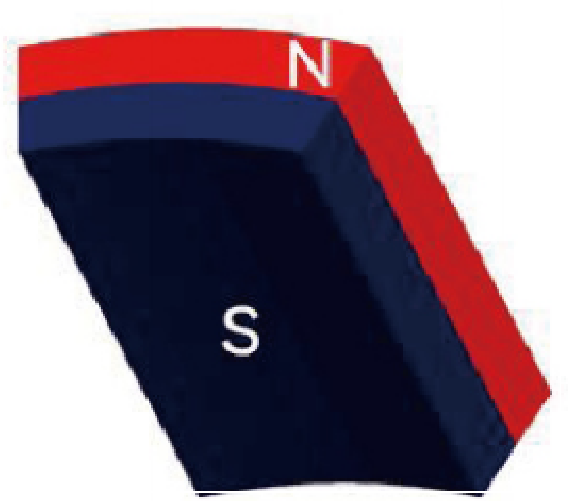
Arc segments are normally magnetized radially, across the arc thickness. Multi-pole patterns are available where a single segment has to carry several poles. For coating, Ni-Cu-Ni covers most indoor motor work; epoxy is specified where the motor sees moisture. Salt-spray performance is quoted per coating in a 12–96 hour window.
Inspection and lead time
Each batch passes a flux-meter performance test, a coating thickness and adhesion check, a salt-spray or humidity test, a pull-force test and a 100 % final inspection before packing. Samples 10–15 days, small batches 20–30 days, mass production 40–60 days. Send the arc drawing — inner radius, outer radius, arc angle, axial length, grade and coating — for a feasibility answer within one business day.
Available magnetisation directions — Arc / tile magnets
The magnetisation direction is fixed when the magnet is magnetised and cannot be changed afterwards, so the direction must be confirmed before production.


Manufacturing capability & measured data
Tolerance
- Standard production
- ±0.05 mm
- Critical dimensions (on request)
- ±0.02 mm
Quoted per dimension against international dimensional quality standards, not as one blanket percentage. ±0.05 mm is the standard band; where a drawing calls for more, critical dimensions are held to ±0.02 mm using grinding or wire-cutting. The final tolerance is confirmed against your drawing before production.
Salt spray
- Duration depends on coating
- 12 – 96 h
Tell us how many hours your application needs and we match the coating to it. The test standard and the hours each coating reaches are confirmed on request.
Lead time
- Sample
- 10 – 15 days
- Small batch
- 20 – 30 days
- Mass production
- 40 – 60 days
Bands are by order type, not a single quantity threshold; exact lead time is confirmed at quotation.
Catalogue range and specialty grades
- Standard catalogue range
- N35–N52 (M–AH series)
- Specialty grade, on request
- N54 / N55
- Designation
- N54 (China) · N55 (international)
Related Products
- Disc N35 N52 10x2 10x3 12x2 12x3 15x2 16x3 Mm
- N52 Ring Magnets — Custom Sintered NdFeB Torus
- Advanced Technology Magnetic Levitation Float
- Powerful Ndfeb Magnet D25mm N52 Disc Countersunk
- Arc Magnet N35 N52 Strong Motor Materials
- N52 Custom Round Industrial Nickel Coated Ndfeb