N52 Strong Holding 10x10x10mm
A block gives the magnetization axis the most freedom
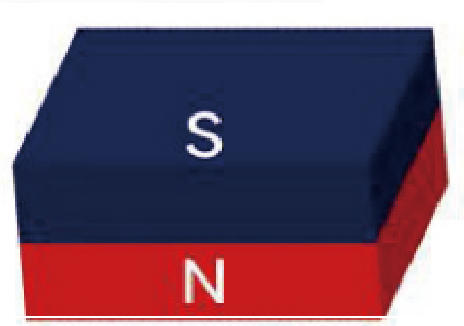
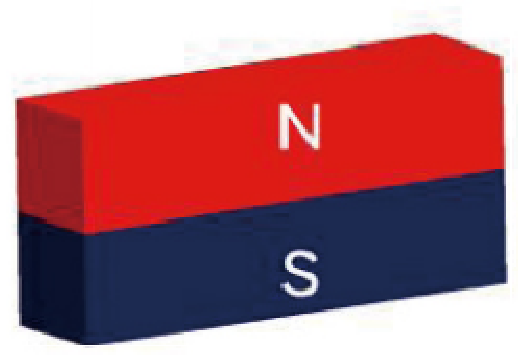
A block is the most flexible shape we make, because the magnetization axis is not tied to the symmetry of the part. A 10 × 10 × 10 mm cube can be magnetized through its thickness (poles on the two 10 × 10 faces), through its width, or diagonally, and each choice produces a different field. Sizes and aspect ratios are produced to drawing, so a block is normally specified by its three dimensions plus the axis you want the poles on.
N52: about 20 % more force, about 20 °C less headroom
At the same pole-face area, moving from N42 to N52 raises flux — the Ansys anchors for a 5 mm thick disc put Br at 13.0 kG for N42 against 14.2 kG for N52, and pull force at 58.18 N against 69.92 N. The cost of that gain is thermal headroom: N52’s maximum operating temperature is 60 °C, while N35–N48 sit at 80 °C. For a holding magnet clamped to a fixture in a normal workshop, N52 is straightforward; where the block sits on a heated machine surface, the arithmetic changes.
Where the 10 × 10 × 10 mm size fits
The 10 × 10 × 10 mm cube is a general-purpose holding and fixture size: small enough to sit in a jig or a sensor housing, large enough to produce a usable holding force. It is quoted on its three dimensions with standard tolerance ±0.05 mm, and ±0.02 mm is available on critical dimensions through grinding or wire-cutting.
Coating and surface
Ni-Cu-Ni is the standard finish and is what most blocks ship with. Black nickel, zinc, tin, gold, silver, black epoxy and phosphating are available where the block is visible in a product, or where it will see moisture. Salt-spray duration is quoted per coating in a 12–96 hour window.
Inspection and lead time
Dimensional check, flux-meter performance test, coating thickness and adhesion, salt-spray or humidity, pull-force and 100 % final inspection before packing. Samples 10–15 days, small batches 20–30 days, mass production 40–60 days; in-stock samples free, freight only. Send the three dimensions, the axis you want magnetized, the grade and the coating — we quote within one business day.
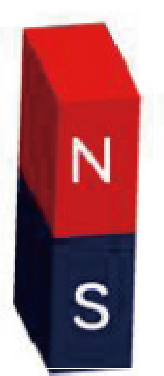
Available magnetisation directions — Block / bar magnets
The magnetisation direction is fixed when the magnet is magnetised and cannot be changed afterwards, so the direction must be confirmed before production.


Manufacturing capability & measured data
Tolerance
- Standard production
- ±0.05 mm
- Critical dimensions (on request)
- ±0.02 mm
Quoted per dimension against international dimensional quality standards, not as one blanket percentage. ±0.05 mm is the standard band; where a drawing calls for more, critical dimensions are held to ±0.02 mm using grinding or wire-cutting. The final tolerance is confirmed against your drawing before production.
Salt spray
- Duration depends on coating
- 12 – 96 h
Tell us how many hours your application needs and we match the coating to it. The test standard and the hours each coating reaches are confirmed on request.
Lead time
- Sample
- 10 – 15 days
- Small batch
- 20 – 30 days
- Mass production
- 40 – 60 days
Bands are by order type, not a single quantity threshold; exact lead time is confirmed at quotation.
Measured N52 properties
- Remanence Br
- 1,420 mT
- Intrinsic coercivity Hcj
- ≥ 955 kA/m
- Max energy product BHmax
- ≥ 390 kJ/m³
- Max operating temperature
- 60 °C
N52 has the highest flux of the sintered grades and the lowest heat tolerance: its maximum operating temperature is 60 °C, against 80 °C for N35–N48. For higher temperatures we move to an H, SH or UH grade and accept slightly lower flux.
Catalogue range and specialty grades
- Standard catalogue range
- N35–N52 (M–AH series)
- Specialty grade, on request
- N54 / N55
- Designation
- N54 (China) · N55 (international)
Related Products
- Disc N35 N52 10x2 10x3 12x2 12x3 15x2 16x3 Mm
- N52 Ring Magnets — Custom Sintered NdFeB Torus
- Full Customized N35 N38 N42h Arc Tile Strong
- Advanced Technology Magnetic Levitation Float
- Powerful Ndfeb Magnet D25mm N52 Disc Countersunk
- Arc Magnet N35 N52 Strong Motor Materials